Conveyor Belts by Industry Application
Whether you run a high-sanitation food bakery, an agricultural grading plant, or a heavy-duty packaging line, Sounil Enterprise engineers custom belting solutions.
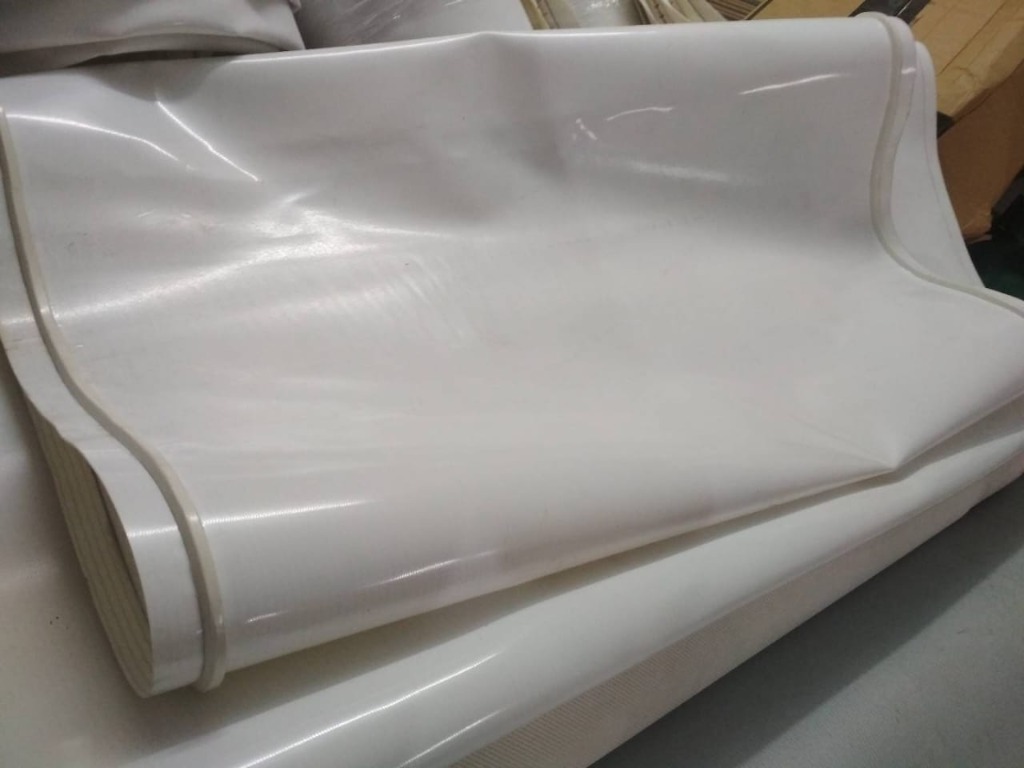
Hygienic, FDA-Approved & Non-Toxic Conveyor Belting
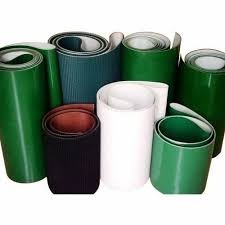
Sanitary white and blue PU/PVC belts designed for dough conveying, biscuit baking lines, chocolates, dairy, confectionery, and meat processing.
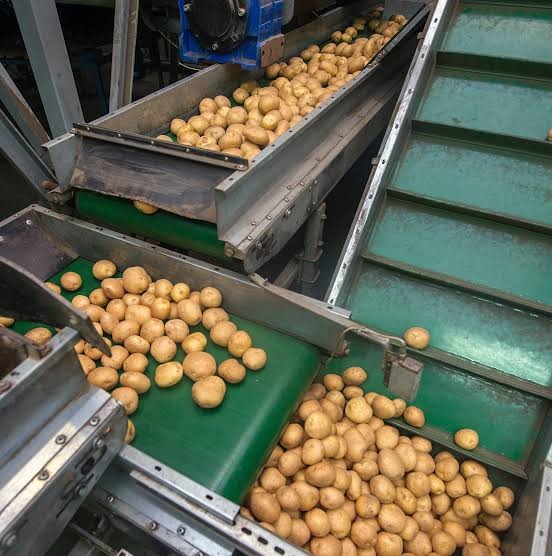
High-Capacity Cleated Elevators & Sorting Conveyor Belts
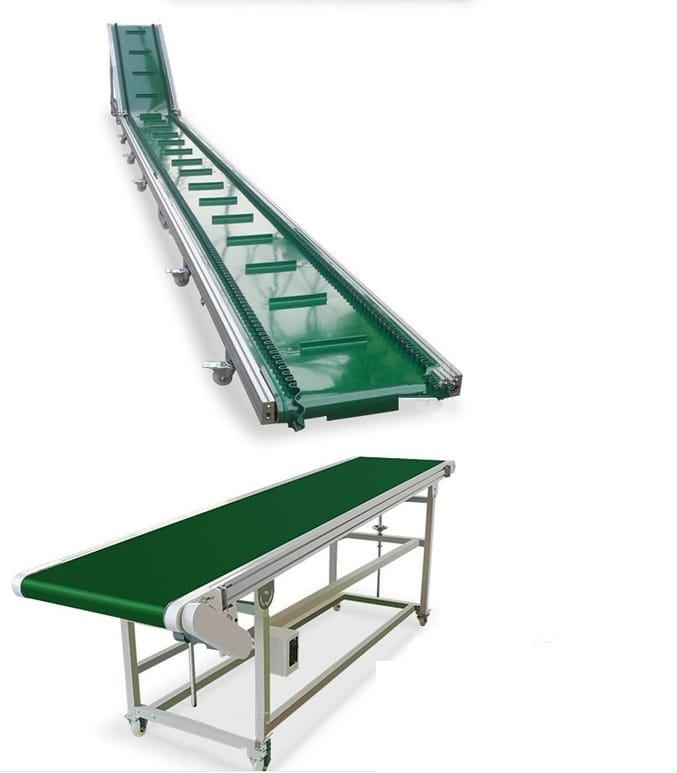
Heavy duty PVC cleated and sidewall belts for potato, onion, tomato grading, seed cleaning, grain elevators, and harvester machinery.
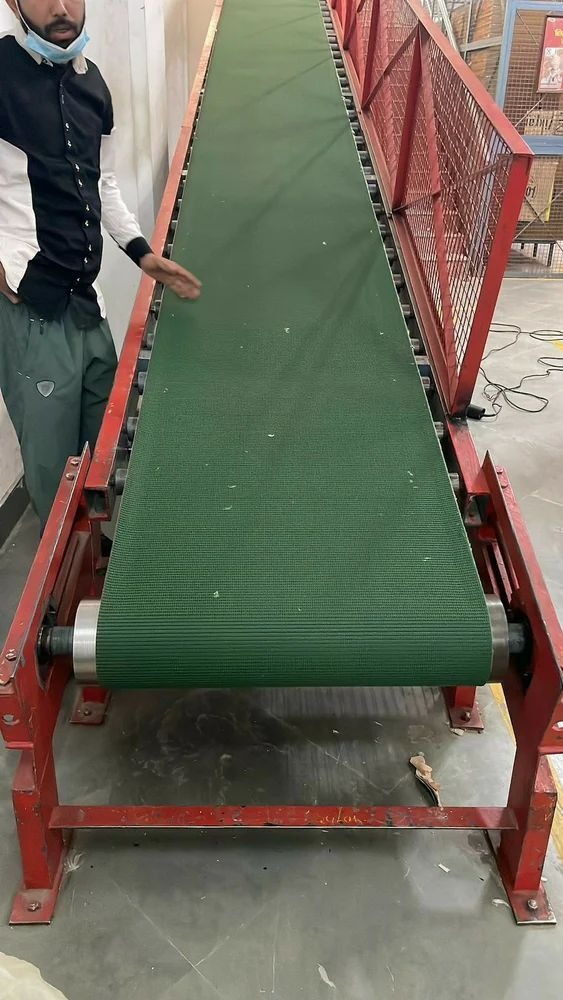
High-Speed, Anti-Static & High-Grip Conveyor Solutions
Rough top, diamond grip, and low-noise flat belts engineered for automated packaging lines, carton sealing machines, and parcel sorting.
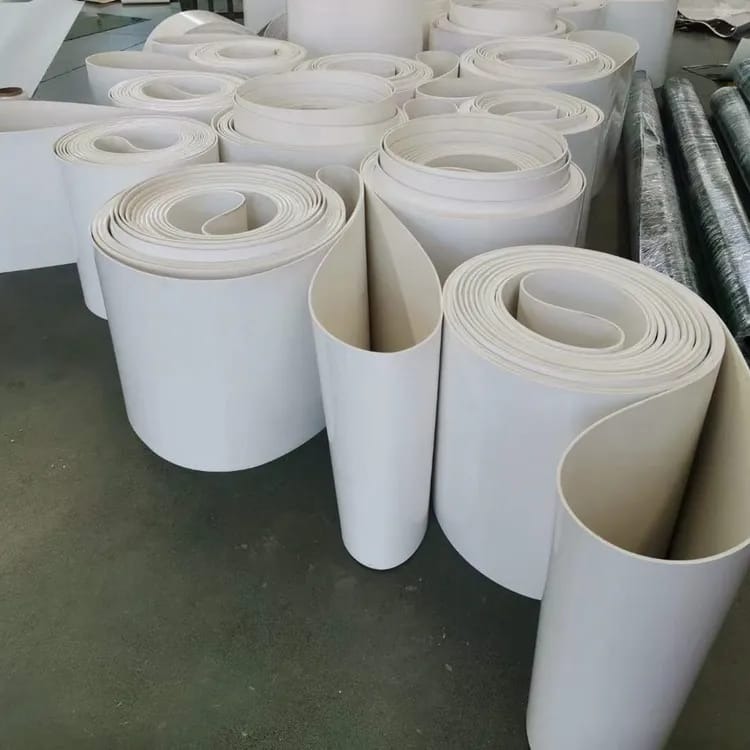
Ultra-Clean, Anti-Static & Chemical Resistant Belts
Precision PU and silicone coated conveyor belts for blister packaging, ampoule inspection, capsule filling, and carton labeling machines.
Heavy Impact, Cut Resistant & Anti-Abrasive Belting
Specialized thick PVC, polyurethane, and grooved belts engineered to endure abrasive ceramic dust, heavy tile glazing lines, and marble cutting tables.
Static-Free, Non-Marking & High-Speed Belting
Anti-static green and black belts for cotton ginning, yarn spinning machines, fabric folding, circular knitting, and garment finishing tables.
Heavy-Duty, Flame Retardant & Low-Noise Belts
High-reliability conveyor belts for airport baggage check-in, X-ray scanning tunnels, carousel claims, and courier hub distribution centers.
Anti-Static, Low Friction & High-Grip Running Belts
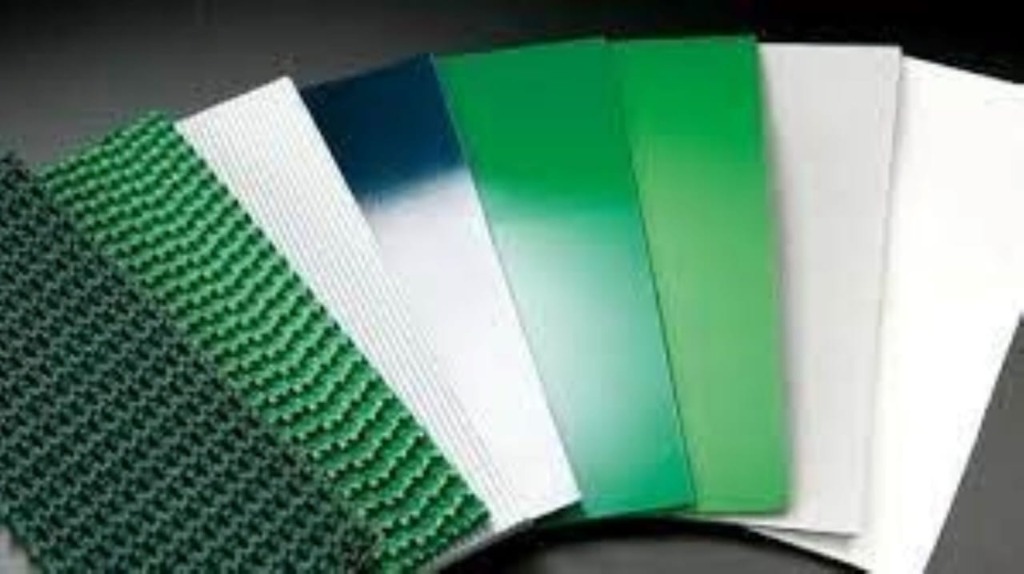
Diamond pattern and golf-grip PVC running belts with whisper-quiet low-friction polyester backing for commercial and home fitness equipment.